

Original TEMI technical documentation. Some language versions differ in dimensions: confirm dimensions, speeds, safety instructions and current specifications with your technical contact before ordering or use.
Bowl, scoop, blade and handle processing
Taking your production possibilities into consideration, we can offer you a complete range of products for your cutlery parts. On the left you see illustrations, showing the use of EP cutlery polishing products. The various processing possibilities with the corresponding buff model have been simplified with a reference table A to N.
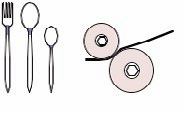
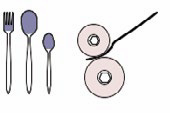
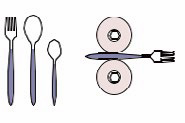
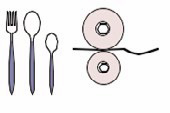
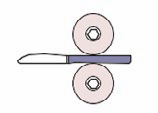
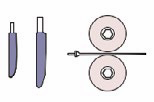
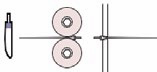
Pre-polishing of the transition area between bowl and handle
e.g. dessert spoons
Top shaft: Type C4/KU, impr. 2E3, profiled, 90 x 35 x 19 hexagonal B
Bottom shaft: Type C4/KU or Type C4/SR, impr. V28, straight, 90x50x19/6 B
Mirror polishing of the transition area between bowl and handle e.g. forks Top shaft: Type D1A/K, qual. NKW, 90 mm Ø, 19 hexagonal J + K Bottom shaft: Type D1A/K, qual. NKW, 100 mm Ø, 19 hexagonal J + K
Pre-polishing of bowl e.g. coffee-spoon Top shaft: Type C4/KU, impr. V31, profiled, 70 x 20 x 19 hexagonal B Bottom shaft: Type C4W/KK, impr. Nr. 3, profiled, 250 x 35 x 70KN C + D
Mirror polishing of bowl e.g. dessert spoon Top shaft: Type D1A/K, qual. NKW, 90 mm Ø, 19 hexagonal J + K Bottom shaft: Type D1C/KK, Polishing-Roller qual. NKW, 250 mm Ø, 19 hexagonal, profiled J + K
Grinding of edges Top and bottom shaft: Type B6/K – 8 ply, impr. LO/10 Ø 120 – 250 mm, 24 hexagonal, grit 120 – 180 N
Pre-polishing of handles all cutlery and flatware parts Top shaft: Type C4/KS, impr. V25, 150 x 50 x 24 hexagonal B + D Bottom shaft: Type C4/KS, impr. V25, 150 x 50 x 24 hexagonal B + D
Mirror polishing of handles all cutlery and flatware parts Top and bottom shaft: Type D1A/K, qual. NKW, 150 mm Ø, 24 hexagonal J + D
Knife processing Pre-polishing of handles For knife handles with poor surface qualities EP-Flap-Wheels Type C28/8 (a mixture of sisal and abrasive flaps) for preparation I + N Top and bottom shaft: Type C8/K mini, impr. 3A or 2E3, 150×24/6 D + H
Mirror polishing of handles Top and bottom shaft: Type D1A/K or D1C, qual. NKW J + K + L
Pre-polishing of blades Top and bottom shaft: Type C11/K, impr. 3a or V23, 250–300 mm Ø G
Mirror polishing of blades Top and bottom shaft: Type D1C, qual. NKW or C32, 250-300 mm Ø J + L
Pre-polishing of hilt Top and bottom shaft Type C4/KU, impr. V25, 70-100 mm Ø x 19 hexagonal B Top and bottom shaft Type C4/K, impr. 2E3, stitched, 350 mm Ø, ∼ 25 mm wide C + F
Mirror polishing of hilt Ideal are the Types D1A/K and D1C, qual. NKW J + L
Scroll the table to view all columns
| EP | Type | Outside diameter | Width | Bores in mm |
|---|---|---|---|---|
| A | Type C3, without center Type C3/KS 15–120 mm Type C3/KU Type C3/SR profiled or straight | 50 – 230 mm | 5mm 15 – 120 mm | 14/6, 19/6, 12/6,14/6, 19/6, 24/6 |
| B | Type C4/KS Type C4/KU Type C4/SR profiled or straight | 50 – 230 mm | 15 – 150 mm | 12/6, 14/6, 19/6, 24/6, 32/6 |
| C | Type C4W/KK | 180 – 300 mm | 30 – 150 mm | 32/6, 45KN, 70KN |
| D | Type C8/K mini | 70 – 230 mm | 10 – 15 mm | 14/6, 19/6, 24/6, 32/6 |
| E | Type C8/K | 180 – 300 mm | 20 mm | 19/6, 24/6, 32/6, 45KN, 70KN |
| F | Type C10 | 180 – 300 mm | 20 mm | 70KN or round |
| G | Type C11 | 180 – 300 mm | 25 mm | 19/6, 24/6, 70KN |
| H | Type C20 | 80 – 1000 mm | 30 – 150 mm | 19/6, 24/6, 32/6, 45KN, 70KN |
| I | Type C28/W | 150 – 1000 mm | 30 – 100 mm | 19/6, 24/6, 32/6, 45KN, 70KN |
| J | Type D1A/K mini | 70 – 230 mm | 9 – 15 mm | 14/6, 19/6, 24/6, 32/6 |
| K | Type D1A/KS, profiled or straight | 70 – 160 mm | 15 – 120 mm | 14/6, 19/6, 24/6 |
| L | Type D1C | 200 – 350 mm | 20 mm | 19/6, 24/6, 32/6 |
| M | Type D1C/KK | 180 – 300 mm | 30 – 150 mm | 32/6, 45KN, 70KN or round |
| N | Type B6/K | 60 – 300 mm | 10 – 20 mm | 14/6, 19/6, 24/6, 32/6 |
- GENERAL RECOMMENDATIONS
- CUTLERY BRUSHES
- BELT-GRINDING
- INFORMATION AND ADVICE
- SPEEDS
✓ Listed in the catalog · — Not specified. Stars retain the original relative rating scale.